Educational Resources
Expertise Explained: Your Guide to Understanding This Key Concept
Understand the concept of expertise through detailed definitions and insights. A must-read for those looking...
TAMFIS NIG LTDRC 8067447CAC ACTIVEFinima, Bonny Island, Rivers State
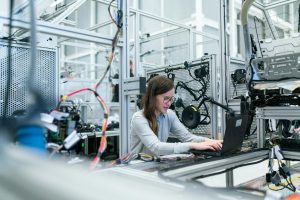
In the complex world of chemical manufacturing, the role of a Maintenance Engineer is pivotal to ensuring operational safety, efficiency, and reliability. At our Denton factory, Ashley stands out as a prime example of dedication and expertise in this field. This article delves into the multifaceted responsibilities of a chemical plant maintenance engineer, highlighting Ashley’s journey, daily tasks, and the critical impact her work has on plant performance. Whether you’re aspiring to enter this profession or seeking insight into industrial maintenance, Ashley’s story offers valuable perspectives.
A Chemical Plant Maintenance Engineer is responsible for overseeing the maintenance, repair, and optimization of equipment and systems within a chemical manufacturing facility. Their role ensures that machinery operates safely and efficiently to meet production goals. This position requires a blend of technical knowledge, problem-solving skills, and the ability to work under pressure in a highly regulated environment.
Maintenance engineers like Ashley coordinate preventive and corrective maintenance tasks to minimize downtime and avoid costly disruptions. They also work closely with operations teams to understand production requirements and tailor maintenance schedules accordingly. Their expertise covers mechanical, electrical, and instrumentation systems critical to plant operations.
Safety is paramount in chemical plants due to the hazardous materials involved. Maintenance engineers must comply with strict safety protocols and industry standards, conducting regular inspections and risk assessments. This proactive approach helps prevent accidents and ensures compliance with environmental and safety regulations.
Ashley’s day begins with a thorough review of the plant’s maintenance schedule and any issues reported by the operations team. She prioritizes tasks based on urgency and potential impact on production. Communication with her team and other departments is essential to coordinate resources and minimize interference with ongoing processes.
Throughout the day, Ashley inspects equipment such as pumps, valves, heat exchangers, and control systems. She uses diagnostic tools and software to identify wear and tear or faults that could lead to failures. When problems arise, Ashley leads troubleshooting efforts, often collaborating with specialists to implement effective solutions promptly.
Ashley also dedicates time to documenting maintenance activities and updating asset management systems. This data helps track the health of equipment, forecast future maintenance needs, and optimize spare parts inventory. Her meticulous record-keeping supports continuous improvement and regulatory compliance.
To excel as a Maintenance Engineer in a chemical plant, a strong foundation in engineering principles is necessary. Ashley holds a degree in Mechanical Engineering, supplemented by certifications in safety and process control. Continuous learning is vital to keep up with technological advancements and evolving industry standards.
Technical skills include proficiency in maintenance management software, understanding of electrical and mechanical systems, and familiarity with instrumentation and control technologies. Ashley’s ability to interpret technical drawings and schematics enables her to diagnose complex issues efficiently.
Soft skills such as communication, teamwork, and problem-solving are equally important. Ashley often liaises between operations, safety, and engineering teams, requiring clear and effective communication. Her analytical mindset helps her anticipate potential problems and devise preventive measures.
One of the primary challenges Ashley encounters is balancing maintenance needs with production demands. Chemical plants operate continuously, so scheduling downtime for repairs requires careful planning to avoid costly interruptions. Unexpected equipment failures can also create high-pressure situations demanding swift action.
Another challenge is maintaining safety in a hazardous environment. Ashley must ensure all maintenance tasks comply with strict safety protocols to protect personnel and prevent environmental incidents. This involves regular training, risk assessments, and the use of personal protective equipment.
Technological complexity is increasing in modern plants, with automation and advanced control systems becoming standard. Ashley continuously upgrades her knowledge to manage these systems effectively, integrating new technologies while maintaining reliability and safety.
Ashley’s proactive maintenance strategies significantly reduce unplanned downtime, allowing the Denton factory to maintain high production rates. By identifying potential failures early, she helps avoid costly repairs and production halts, contributing directly to the plant’s profitability.
Her commitment to safety ensures that equipment operates within safe parameters, reducing the risk of accidents and environmental hazards. Ashley’s rigorous inspections and adherence to safety standards protect both employees and the surrounding community.
Moreover, Ashley’s thorough documentation and data analysis enable continuous improvement initiatives. This data-driven approach helps optimize maintenance schedules and resource allocation, fostering a culture of efficiency and reliability within the plant.
Ashley’s career trajectory highlights the diverse opportunities available to maintenance engineers in the chemical industry. Starting as a junior technician, she advanced through roles involving greater responsibility and technical complexity, supported by ongoing professional development.
Maintenance engineers can specialize in areas such as reliability engineering, asset management, or safety engineering. Leadership roles like Maintenance Manager or Plant Engineer are also attainable with experience and demonstrated expertise.
Industry trends emphasize the integration of digital technologies like predictive maintenance and IoT (Internet of Things). Ashley is actively involved in adopting these innovations, which not only enhance plant performance but also open new avenues for career advancement.
Ashley advises aspiring maintenance engineers to build a strong educational foundation in engineering, preferably with a focus on mechanical, electrical, or chemical disciplines. Gaining practical experience through internships or apprenticeships in industrial settings is invaluable.
She emphasizes the importance of developing both technical and soft skills. Understanding plant operations, safety regulations, and maintenance management systems is essential, as is the ability to communicate effectively and work collaboratively.
Continuous learning is key in this evolving field. Ashley recommends pursuing certifications related to safety, process control, and maintenance technologies, as well as staying updated on industry best practices and emerging trends.
The role of maintenance engineers like Ashley is evolving with advancements in technology and increasing regulatory demands. Predictive maintenance, powered by data analytics and machine learning, is becoming a standard practice to anticipate equipment failures before they occur.
Sustainability and environmental considerations are also shaping maintenance strategies. Engineers are tasked with optimizing energy efficiency and reducing waste, aligning plant operations with global sustainability goals.
Ashley is excited by these developments, viewing them as opportunities to enhance plant performance and safety. The integration of smart technologies promises to make maintenance more precise and less disruptive, reinforcing the critical role of engineers in the chemical industry’s future.
Ashley’s journey as a Maintenance Engineer at the Denton chemical plant highlights the indispensable role these professionals play in maintaining operational excellence and safety. Her expertise, dedication, and forward-thinking approach ensure that the plant runs smoothly, meeting production targets while adhering to stringent safety standards. As the chemical industry embraces new technologies and sustainability goals, maintenance engineers like Ashley are positioned at the forefront of innovation and reliability. For those considering a career in this dynamic field, Ashley’s story underscores the importance of technical knowledge, continuous learning, and a commitment to safety and teamwork.
Keep reading
Educational Resources
Understand the concept of expertise through detailed definitions and insights. A must-read for those looking...
Mechanical
Predictive Maintenance (PdM) has revolutionized the way industries maintain their equipment, shifting fr...
Mechanical
Venezuela, once one of Latin America's wealthiest nations due to its vast oil reserves, has experie...
TAMFIS NIG LTD
Electrical and instrumentation engineering, bid preparation and consulting, IT and software.